Control the costs that never appear on the purchase order
Manufacturing cost management is not simply a search for the lowest component price. Procurement and operations teams also need visibility into inventory carrying cost, maintenance timing, obsolescence exposure, wrong-part risk and the production impact of delayed recovery.
This guide presents a practical decision framework for industrial automation spares. It helps teams compare what it costs to hold a critical spare with what it could cost to wait for a failure, source the wrong revision or accept an unrealistic lead time.
Four cost pools belong in one decision
Capital tied up, storage, ageing, preservation and the chance that a stocked item no longer matches the installed base.
Labour, planned shutdown access, test equipment, repair scope and the evidence required to return an asset to service.
Lost throughput, idle labour, recovery sequencing, quality losses and expedited logistics during an interruption.
Wrong suffixes, incomplete revisions, unsuitable condition, uncertain lead times and unverified substitution.
Why unit price is only one line in the cost model
A low quoted price can still produce a high total cost when the part number is incomplete, the condition is unclear, documentation is missing or the delivery window does not match the shutdown plan.
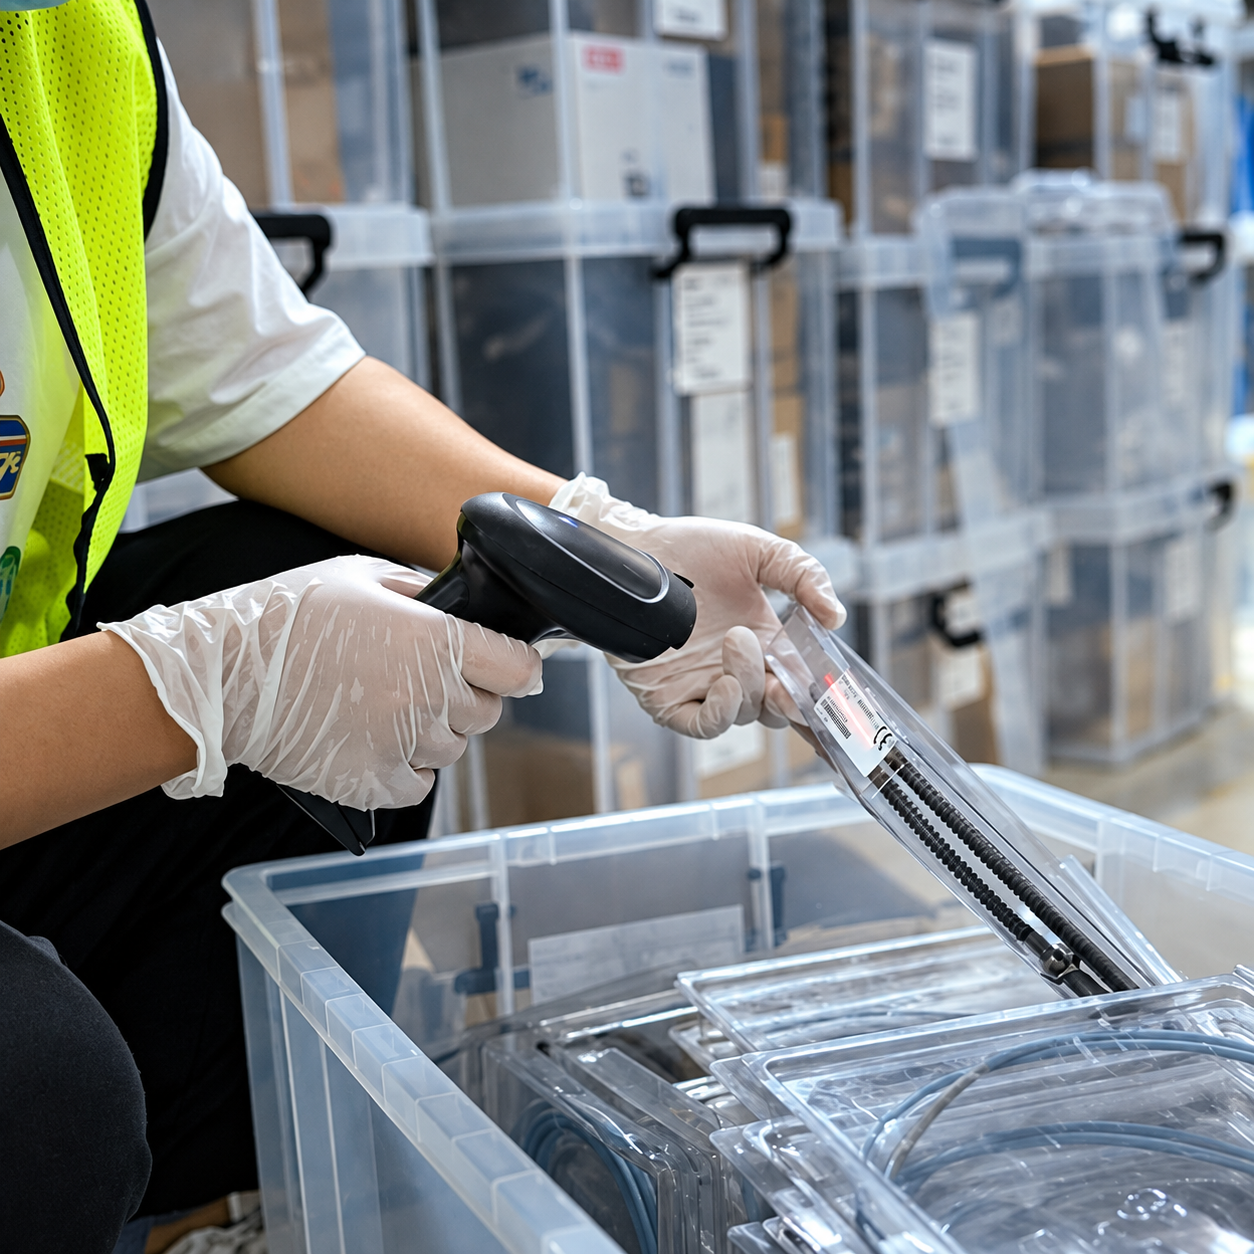
Before comparing offers, standardise the evidence requested from every supplier: complete manufacturer part number, suffixes, stated condition, quantity, test or inspection scope, written lead time, warranty terms and delivery destination.
| Cost signal | Evidence to request | Decision question |
|---|---|---|
| Price variance | Condition, inclusions, warranty and freight basis | Are the quotations genuinely comparable? |
| Lead-time risk | Stock status, dispatch point and written availability | Does the date protect the maintenance window? |
| Wrong-part risk | Full part number, suffix, revision and nameplate image | Has the exact installed requirement been matched? |
| Lifecycle risk | OEM notices, installed-base data and migration status | Should the team stock, repair or plan replacement? |
Stock by consequence, not by habit
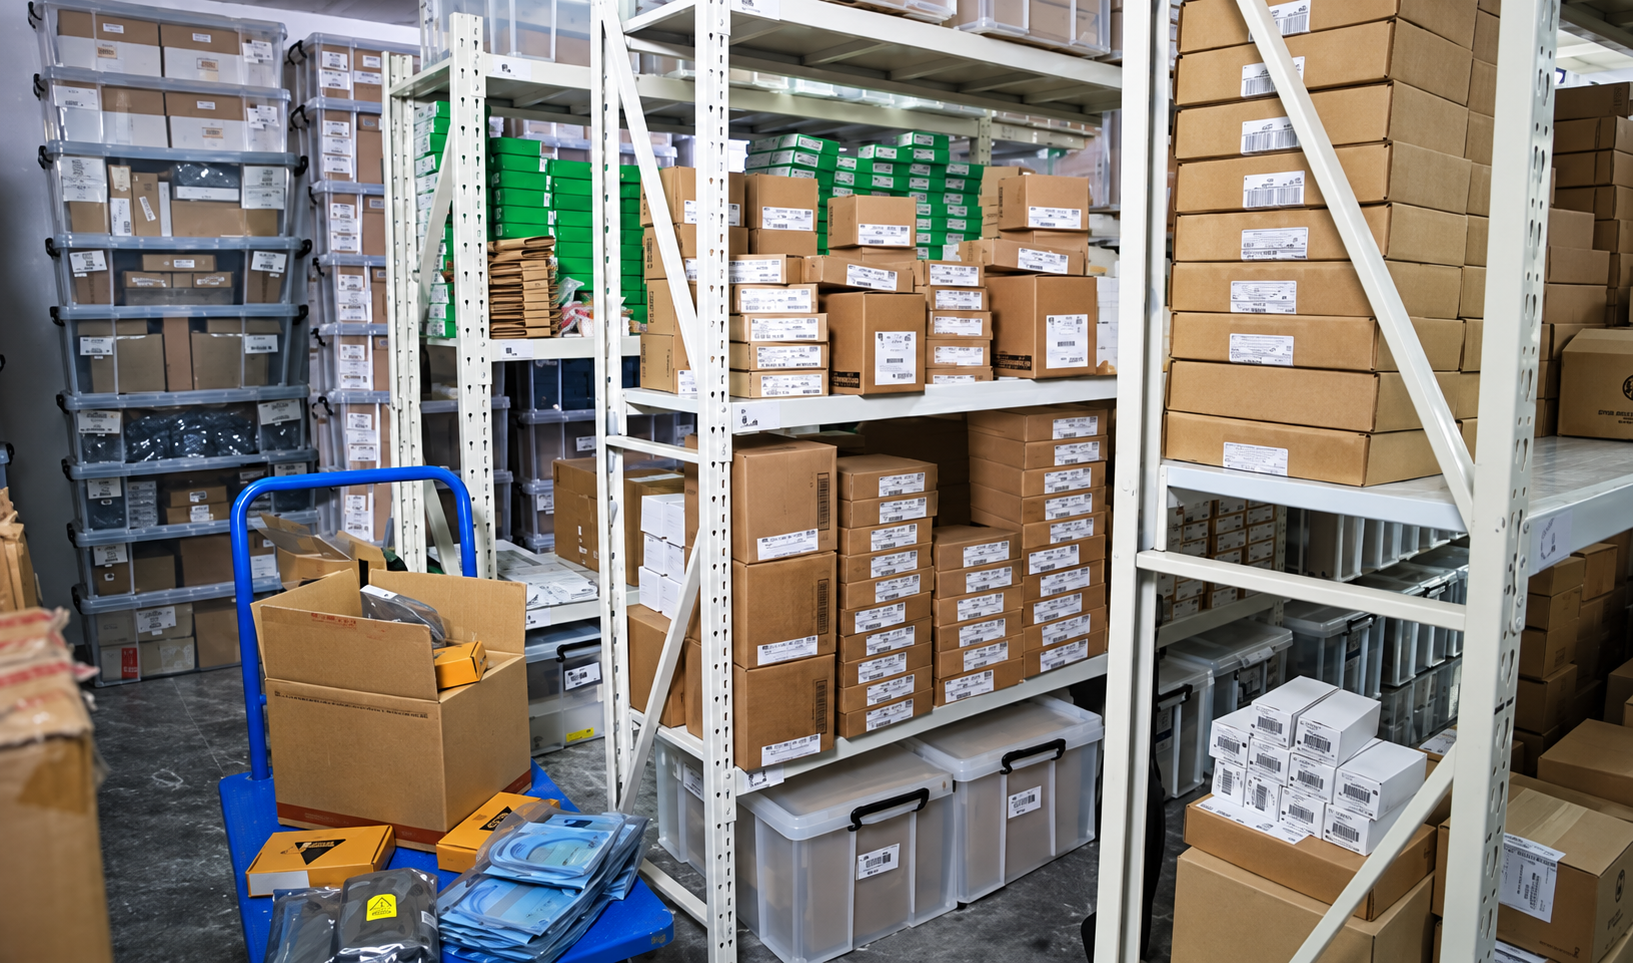
Critical-spares planning should connect the probability of failure with the consequence of waiting. A rarely used module may still deserve protection if it can stop a bottleneck asset and has a long or uncertain replacement route.
Conversely, buying every available obsolete part can create stranded stock. Review installed quantity, commonality across lines, historical consumption, shelf-life or preservation needs, repair options, substitution constraints and migration timing.
IAS 2 provides the accounting framework for inventory cost and write-downs. Operational teams still need an engineering view of why a spare is held and what risk it is intended to control.
Consider a verified strategic spare, preservation plan and defined reorder trigger.
Confirm supplier capacity and emergency logistics rather than assuming immediate supply.
Use commonality, repairability and installed quantity to decide whether holding stock is justified.
Buy against a clear requirement and monitor lifecycle changes without automatically increasing stock.
Budget around failure modes and decision windows
A NIST manufacturing study reported that establishments relying heavily on reactive maintenance were associated with materially higher downtime, defects, lost sales and maintenance-related inventory increases. The practical lesson is not that one maintenance method fits every asset; it is that the mix should be deliberate, measured and aligned to consequence.
Exact module identification is a cost-control step
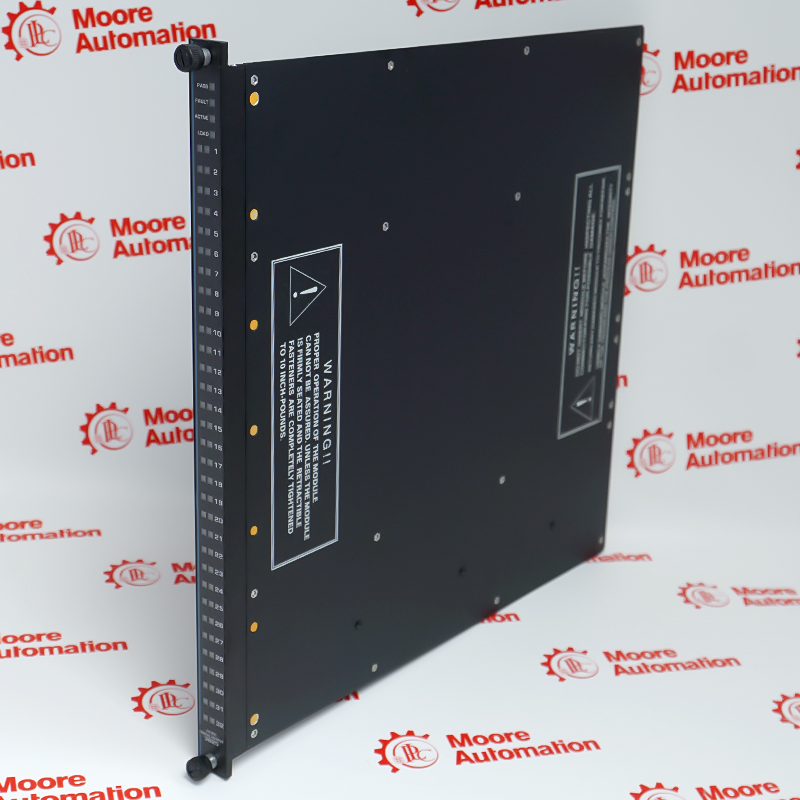
The short Moore Automated video below shows an ICS Triplex T8431 analogue input module. A product video does not prove application compatibility, but it can support the evidence package used to confirm physical identity, visible condition and the precise item being discussed.
Video context: product footage supports visual identification only. Final suitability depends on the complete part number, system requirements, agreed condition and written quotation.
Turn a spare-parts request into a cost decision
Asset, failure mode, production consequence, required date and acceptable operating alternatives.
Manufacturer, full part number, suffix, revision, quantity and installed-system context.
Condition, evidence, warranty, lead time, logistics basis and technical exclusions.
Document why the item was stocked, repaired, expedited, deferred or included in a migration plan.
Components commonly included in critical-spares reviews
Evidence before commitment
Guidance used for this article
Source names are presented as plain text. No third-party hyperlinks are embedded in this section.
- U.S. Department of Energy — Operations and Maintenance Best Practices: A Guide to Achieving Operational Efficiency.
- National Institute of Standards and Technology — Research on the manufacturing impact of advanced machinery maintenance.
- ISO 55000:2024 — Asset management vocabulary, overview and principles.
- IFRS Foundation, IAS 2 Inventories — Inventory cost, measurement and write-down principles.
- Moore Automated operational guidance — Part-number verification, condition disclosure and written quotation practices.
Build a cost-aware critical-spares plan
Send the manufacturer, complete part number, quantity, destination, required date and the asset consequence you are trying to control. Moore Automated can confirm available product information, stated condition, lead time and applicable warranty in writing.
Manufacturing cost management FAQ
How should a manufacturer estimate downtime cost?
Use a documented range based on the affected production rate, contribution margin, idle labour, quality loss, restart requirements, contractual exposure and recovery time. Separate known data from assumptions and avoid presenting a generic industry average as a guaranteed site-specific loss.
When is it reasonable to hold an obsolete automation spare?
It may be reasonable when the part supports a critical asset, failure consequence is high, replacement lead time is long or uncertain, and compatibility has been verified. The decision should also consider preservation, shelf life, repairability, migration timing and the risk of stranded inventory.
How can procurement compare quotations fairly?
Ask every supplier to state the complete part number, suffix, revision where applicable, product condition, quantity, inspection or test scope, dispatch status, lead time, freight basis, warranty and exclusions. Unit prices should be compared only after these fields are aligned.
Does a product video prove that a module is compatible?
No. A video may support visible identification, but compatibility depends on the complete manufacturer part number, installed architecture, firmware or revision requirements, application data and engineering approval where required.
What information helps Moore Automated prepare a quotation?
Provide the manufacturer, complete part number, all suffixes, quantity, preferred condition, destination country, required date and a clear nameplate photograph if available. Sharing the installed system or planned maintenance window can reduce clarification cycles.
Can Moore Automated confirm delivery and warranty before purchase?
Availability, lead time, stated condition and applicable warranty should be confirmed in the written quotation for the specific item. Dispatch timing depends on confirmed stock, order processing, destination and the selected logistics service.
Leave Your Comment